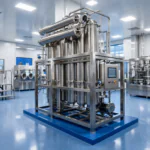


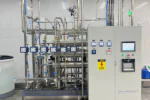
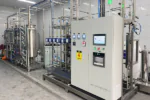
Pharma Purified Water System
♦ Main Application:
Applications: Pharmaceutical manufacturing, biotechnology, and healthcare production.
Standards: Designed to meet applicable USP / EP Purified Water requirements with GMP-oriented engineering.
Pharmaceutical Purified Water System Overview
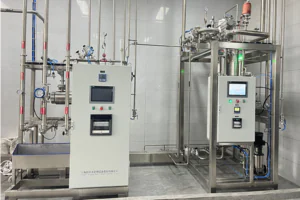
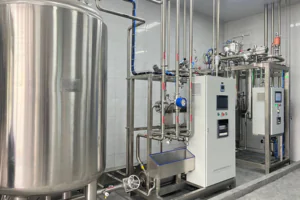
CHONGYANG WATER designs and manufactures customized pharmaceutical purified water systems for pharmaceutical manufacturing, biotechnology facilities, and GMP-regulated production environments.
Our pharmaceutical water treatment systems integrate pretreatment, reverse osmosis (RO), optional electrodeionization (EDI), UV treatment, and sanitary storage and distribution to produce consistent, high-quality Purified Water (PW).
Each system is engineered according to feed water quality, production capacity, operating conditions, and applicable USP and European Pharmacopoeia (EP) requirements, with documentation support for pharmaceutical qualification and validation.
Key System Capabilities
Pharmaceutical Purified Water Generation Process
A reliable pharmaceutical water purification system combines suitable pretreatment, membrane separation, optional ionic polishing, and microbial control technologies.
Typical Double-Pass RO + EDI Process
|
Raw Water
|
→ |
Multi-Media Filter
|
→ |
Activated Carbon Filter
|
→ |
Water Softener
|
→ |
Chemical Dosing
|
→ |
Cartridge Filter
|
→ |
First-Pass RO
|
→ |
Second-Pass RO
|
→ |
EDI
|
→ |
UV Treatment
|
→ |
PW Storage Tank
|
→ |
Distribution Loop
|
→ |
Points of Use
|
→ |
Return to PW Tank
|
Scroll horizontally to view the complete process on mobile devices.
This is a typical configuration. The actual process may vary according to raw water analysis, target water quality, and project requirements.
Pretreatment System
Pretreatment protects RO membranes and maintains stable feed water conditions. Depending on source water quality, it may include multi-media filtration, activated carbon filtration, water softening, chemical dosing, and cartridge filtration. Additional treatment can be incorporated for iron, manganese, or excessive hardness.
Reverse Osmosis (RO)
Reverse osmosis is a primary purification technology used in pharmaceutical reverse osmosis systems. RO membranes reduce dissolved salts and a wide range of other contaminants. CHONGYANG provides single-pass and double-pass RO configurations with suitable pumps, membrane elements, automated flushing, and online process monitoring.
Double-pass RO can be selected when additional ionic removal or improved EDI feed water quality is required.
Electrodeionization (EDI)
EDI combines ion-exchange materials, selective membranes, and electrical power for continuous ionic polishing. An appropriately designed RO EDI purified water system can achieve stable low-conductivity water without routine chemical regeneration of conventional mixed-bed ion exchange resins.
EDI selection depends on RO permeate quality, dissolved carbon dioxide, hardness, silica, and other operating conditions.
UV Treatment and Microbial Control
UV treatment may be used for microbial control or TOC reduction, depending on the selected wavelength and system configuration. Hot water sanitization, ozone sanitization, hygienic piping, continuous circulation, and routine monitoring can also be incorporated according to the approved microbial control strategy.
Technical Specifications
Typical System Configuration
| Parameter | Specification |
|---|---|
| Product | Pharmaceutical Purified Water System |
| Production Capacity | 500–50,000 L/h |
| Feed Water | Municipal Water / Well Water |
| Pretreatment | Customized MMF / ACF / Softening |
| RO Configuration | Single-Pass / Double-Pass |
| EDI | Optional |
| UV Treatment | Application-Specific |
| Ultrafiltration | Optional |
| PW Storage Tank | SS316L |
| Distribution Piping | SS316L |
| Surface Finish | Ra ≤0.6 / ≤0.8 μm, as specified |
| Sanitization | Hot Water / Ozone |
| Control System | PLC + HMI |
| SCADA Integration | Optional |
| Documentation | FAT / SAT / Qualification Support |
Final equipment configuration and specifications are determined by the approved User Requirement Specification (URS).
Purified Water Quality and Monitoring
| Parameter | Design Requirement |
|---|---|
| Conductivity | Applicable USP / EP PW Specifications |
| TOC | Typically NMT 500 ppb |
| Microbial Quality | Project-Specific Alert and Action Limits |
| Endotoxin | Where Required by Application |
| Online Conductivity | Available |
| Online TOC | Optional |
| Flow / Pressure / Temperature | Online Monitoring Available |
| Qualification | DQ / IQ / OQ / PQ Support as Agreed |
Final water quality compliance must be demonstrated through appropriate testing, qualification, monitoring, and system operation.
GMP Hygienic Design and Construction
Pharmaceutical purified water systems require hygienic engineering to reduce contamination risks and support effective cleaning, sanitization, and long-term operation.
SS316L Sanitary Construction
CHONGYANG provides sanitary storage and distribution systems with available features including:
- SS316L product-contact tanks and piping
- Electropolished surfaces
- Hygienic diaphragm valves and fittings
- Automatic orbital welding
- Drainable piping arrangements and controlled dead-leg design
- Material traceability, passivation and surface finish documentation
- Sanitary tank vent filtration
Design details are established according to the approved URS and applicable hygienic engineering requirements.
Purified Water Storage and Distribution
The purified water storage and distribution system is designed to maintain water quality between generation and points of use. A typical configuration includes a sanitary PW tank, circulation pump, distribution piping, return line, monitoring instruments, and suitable sanitization provisions.
Loop sizing and circulation conditions are determined according to point-of-use demand, pipe length, hydraulic requirements, and microbial control strategy.
PLC Automation and Online Monitoring
CHONGYANG systems can be equipped with PLC and HMI controls for automatic operation and process monitoring.
- Automatic startup, shutdown, and RO flushing
- Conductivity, flow, pressure, and temperature monitoring
- Tank level and pump control
- Alarm recording and equipment status display
- Automated sanitization sequences
- Optional SCADA communication
Electronic records, audit trails, and 21 CFR Part 11-related functionality can be incorporated according to defined project requirements.
Key Features and Advantages
System configuration is selected according to feed water analysis, target water quality, capacity, and operating conditions.
Suitable pretreatment, RO, optional EDI, and online monitoring support consistent system performance.
SS316L sanitary components, appropriate surface finishing, and hygienic piping support water quality management.
PLC and HMI controls support process monitoring, operational consistency, and alarm management.
Generation equipment can be supplied together with sanitary storage tanks and distribution systems.
Technical drawings, FAT/SAT documentation, and qualification support are available according to project scope.
Applications in Pharmaceutical Manufacturing
CHONGYANG purified water systems for pharma can be configured for:
- Pharmaceutical formulation and manufacturing
- Biotechnology production facilities
- Non-sterile pharmaceutical manufacturing
- Equipment cleaning and rinsing
- Vaccine and sterile manufacturing support applications
- Medical device manufacturing
- Research and development laboratories
- Nutraceutical and healthcare production
The required pharmaceutical water grade must be selected according to the intended application. Purified Water (PW) and Water for Injection (WFI) are not interchangeable.
Engineering Documentation and Project Support
CHONGYANG provides customized engineering and technical support throughout the pharmaceutical water treatment project.
| Project Stage | Available Support |
|---|---|
| Requirement Review | URS Review and Technical Clarification |
| Process Design | Process Flow Diagram and P&ID |
| Equipment Engineering | Configuration and Layout Drawings |
| Manufacturing | Fabrication and Assembly |
| Factory Testing | FAT |
| Installation & Commissioning | Technical Guidance and SAT Support |
| Qualification | DQ / IQ / OQ / PQ Support as Agreed |
| After-Sales | Maintenance Guidance and Spare Parts |
Frequently Asked Questions
1. What is a pharmaceutical purified water system?
A pharmaceutical purified water system is an integrated treatment solution designed to produce water meeting applicable Purified Water specifications for pharmaceutical manufacturing, cleaning, and process applications. It typically combines pretreatment, RO, optional EDI, microbial control, and sanitary storage and distribution.
2. How does an RO EDI purified water system work?
Reverse osmosis reduces dissolved salts and other contaminants from pretreated water. EDI provides additional ionic removal through ion-exchange materials, selective membranes, and electrical power. The combined process supports stable low-conductivity water production when properly designed and operated.
3. Is double-pass RO necessary for pharmaceutical purified water?
Not always. Single-pass RO, double-pass RO, and RO + EDI configurations may be suitable depending on feed water quality, target water specifications, and operating requirements.
4. Can pharmaceutical purified water systems meet USP and EP requirements?
Yes. A properly designed, operated, monitored, and qualified system can produce water meeting applicable USP and EP Purified Water specifications. Compliance must be demonstrated through the required water quality testing and qualification activities.
5. What is the difference between Purified Water and Water for Injection?
Purified Water (PW) and Water for Injection (WFI) are different pharmaceutical water grades. WFI has additional quality requirements and requires an appropriate, qualified generation and distribution approach. A standard PW system should not be assumed to produce WFI.
6. What information is required for a quotation?
To prepare a customized technical proposal, please provide:
- Feed water analysis and target water quality
- Required production capacity and daily operating hours
- Storage tank capacity
- Number of points of use
- Distribution loop length and layout
- Sanitization requirements
- Available utilities
- Required qualification documentation
Why Choose CHONGYANG WATER?
CHONGYANG WATER provides customized pharmaceutical purified water generation, storage, and distribution solutions for international pharmaceutical manufacturers, engineering contractors, and system integrators.
Our capabilities include RO and EDI purification systems, SS316L sanitary construction, PLC automation, engineering documentation, factory testing, and international technical support.
We focus on practical engineering solutions based on actual feed water conditions, production requirements, and customer specifications.
Request a Pharmaceutical Purified Water System Quotation
Looking for a reliable pharmaceutical purified water system manufacturer?
CHONGYANG WATER provides customized RO, EDI, purified water generation, storage, and distribution solutions for pharmaceutical manufacturing facilities.
Send us your URS, feed water analysis, and required production capacity to receive a customized technical proposal and quotation.